Stage 4 of 5 · Part of Battery Recycling
Mechanical Battery Recycling
In this mechanical battery recycling stage, dismantled batteries are processed—through shredding, crushing, or milling—to break them down into smaller fragments. The aim is to isolate key material groups such as metals, plastics, electrolyte and black mass for further refinement.

Material separation—commonly referred to as mechanical recycling—is a standalone process that takes in charged or discharged batteries and outputs black mass along with sorted metal and plastic fractions.
The process begins with shredding to break open the battery structure and expose internal components. Shredding is often done in water or under inert atmosphere for safety. Electrolyte is removed by evaporation or pyrolysis.
After shredding, physical separation techniques such as milling, sieving, air classification, and magnetic separation are used to isolate black mass (containing anode and cathode materials) from other streams. Graphite can optionally be removed through flotation.
- IN
- (Discharged) packs, modules, cells
- Cell production scrap (jelly rolls, cathode foils)
- OUT
- Cu, Al, Fe fractions
- Plastics
- Electrolyte
- Black mass
- Graphite
4.1 Battery Shredding
- IN
- (Discharged) Battery Packs
- (Discharged) Battery Modules
- (Discharged) Battery Cells
- OUT
- Battery Fractions Approximately 3 cm × 3 cm or Smaller
- TECH
- Battery Material Shredder:
- single step
- multi-stage process
EA Partner Solutions: ANDRITZ AG
Battery packs, modules, cells, and production scrap such as coated foils or jelly rolls are fed into a shredder, where powerful blades break the material into smaller pieces. This process exposes the internal components, enabling the separation of valuable materials in later stages. Shredding can be done in a single step or as a multi-stage process. In multi-stage setups, a rough shredder is used first, followed by finer shredders that progressively reduce the particle size.
A typical shredding system consists of several key components: an automatic feeding system, shredding chamber, knives, optional sieve, outfeed system, safety system, off-gas treatment or filtration unit, and a control cabinet.
The feeding system is often a cleated conveyor belt. The cleat size should be selected based on the dimensions of the infeed material to ensure stable transport into the shredder.
Additional process considerations
- Knife selection and turning speed are critical to ensure optimum black mass recovery. Improper knife selection or rotation speed can lead to pocket formation, where current collector foils are folded or crumpled in a way that traps black mass inside, making it inaccessible for downstream separation processes.
- Outfeed systems vary depending on the material and layout and can include screw conveyors, drag chain conveyors, or similar equipment tailored to the throughput and material characteristics.
Shredding with water
In this setup, batteries are either submerged in water during shredding or sprayed with water to suppress sparks and cool the materials. This method reduces the risk of fire, though sparks can still occur under water, and fires may still happen with surface sprinkling only. To operate such a system, a water recirculation and treatment system is required. Electrolyte accumulates in the water over time, so a bleed and concentration control system is needed. Additionally, black mass fines build up in the water and must be removed—typically with a filter press to prevent loss and operational issues. For water-based shredding, deep discharge is not required, but a minimum discharge level is typically recommended for safety.
Shredding in an inert atmosphere
In this approach, batteries are shredded in a nitrogen-filled chamber to displace oxygen and minimize the risk of ignition. Because oxygen must be kept out, continuous processes must be adapted into batch-wise loading, typically using an airlock system to introduce material safely. Deep discharge is strongly recommended when shredding under inert gas. A fully charged battery shredded in this environment could still catch fire, so an automatic fire suppression system is required as a precaution.
Field challenges
Risk of material contamination and reduced black mass purity
During shredding, all battery materials—including active materials, current collectors, plastics, and binders—are mixed together. These must be separated in downstream processes. However, depending on the separation technologies used, some materials can be recovered more efficiently than others. Particular attention should be paid to copper and aluminum, which originate from the anode and cathode foils. If not properly separated, these metals can contaminate the black mass, reducing its purity and value.If batteries with different chemistries (e.g., NMC, LFP, NCA, LCO) are shredded together, the resulting black mass will be cross-contaminated, lowering its value and reducing the efficiency of downstream hydrometallurgical recovery processes.
Safety risks from fire, toxic gases, and fine dust from shredding
Battery shredding introduces major safety hazards, including the risk of fire, harmful gas release, and airborne particulate matter. These risks are caused by residual electric charge, flammable electrolyte solvents, and reactive salts. Additionally, fine dust generated during shredding can pose health hazards to workers and environmental risks. Proper safety measures—such as fire suppression, gas filtering, dust collection systems, and PPE—are essential to mitigate these risks.
Wear and tear on shredding equipment
Shredding lithium-ion batteries places significant mechanical and chemical stress on key components—particularly the knives. Hard metals like stainless steel and chemically aggressive substances such as electrolyte salts contribute to rapid degradation. As a result, shredders require frequent maintenance, reducing overall operational uptime and increasing costs.
Solutions for this step
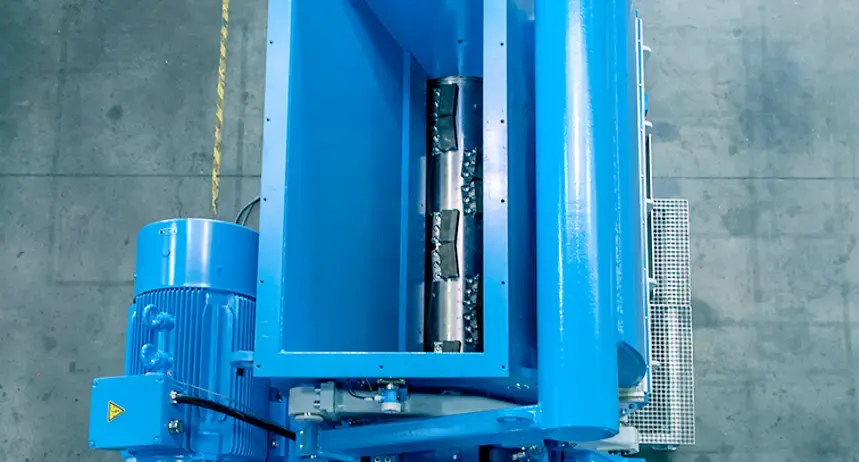 The ADuro G single-shaft shredder enables efficient material processing. Guillotine shear, adjustable knife gap, and granulation screen ensure high throughput and defined particle size.
ANDRITZ AG · Battery Material Shredder
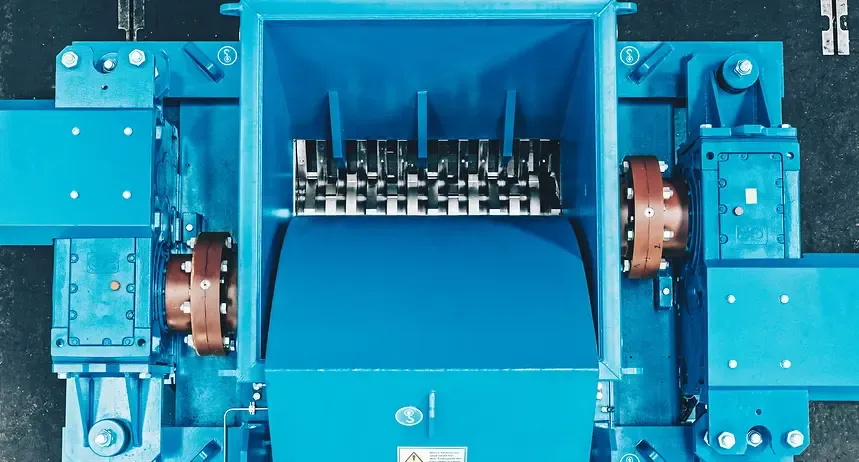
Rotary Shear ADuro C Pre-Shredder
The slow-running, twin-shaft rotary shear pre-shredder ADuro C operates at variable speeds, using intermeshing blade discs and a pendulum pusher to boost throughput.ANDRITZ AG · Battery Material Shredder
4.2 Electrolyte Removal
- IN
- Shredded battery with electrolyte solvents
- OUT
- Shredded battery without electrolyte solvents
- TECH
EA Partner Solutions: ANDRITZ AG, Riedhammer GmbH
After the battery has been shredded, the resulting shreds are dried to remove residual electrolyte solvents and, depending on the temperature, possibly degrade active material binders such as polyvinylidene fluoride (PVDF). Drying is essential for ensuring the safety and efficiency of subsequent processing steps—by preventing clumping and improving material flow during separation.
Common drying technologies include rotary dryers or kilns, vacuum dryers, and conventional ovens.
The selected drying temperature influences the design of the off-gas treatment system, as higher temperatures may lead to more aggressive or hazardous vapors.
Field challenges
Process mismatch between continuous shredding and batch vacuum drying
Vacuum drying is typically a batch process, whereas shredding is a continuous process. This creates a mismatch in throughput and may require buffering systems in between, introducing inefficiencies and additional complexity in the overall process flow.
Confidential electrolyte mixture
The drying process needs to be designed to fit different electrolyte mixtures (expecting to process different batteries). In addition to that each electrolyte solvent mixture is kept confidential by the cell producer. Especially because of that processing parameter flexibility is required to ensure that all battery shreds are properly dried.
Incomplete evaporation of high-boiling solvents (e.g. ethylene carbonate)
Effective electrolyte removal depends heavily on drying temperature. Higher temperatures improve solvent evaporation, while lower temperatures increase energy efficiency—so finding the right balance is critical. Typical electrolyte mixtures include solvents like dimethyl carbonate (DMC), ethyl methyl carbonate (EMC), and ethylene carbonate (EC). Among these, ethylene carbonate has the highest boiling point. If drying temperatures are too low, EC may not fully evaporate, leaving behind residues that interfere with downstream processing.
Aggressive solvent vapors can damage seals and components
During drying, battery solvents evaporate and are treated as off-gases in specialized systems. These vapors—including decomposition products from electrolyte salts like lithium hexafluorophosphate (LiPF₆) or fluorinated binders such as polyvinylidene fluoride (PVDF) and polytetrafluoroethylene (PTFE)—are highly aggressive toward materials. Components such as vacuum pump seals and any materials in contact with the off-gases must be carefully selected to ensure durability and system reliability.
Solutions for this step
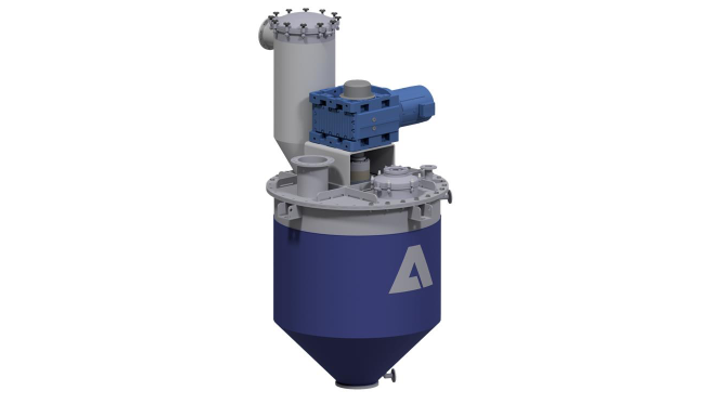 The GHD-LIB 4000 is a vertical deep vacuum dryer that can dry a 4,000-liter batch at a time. The design has been iteratively optimized for drying lithium-ion batteries.
ANDRITZ AG · Battery Material Dryer
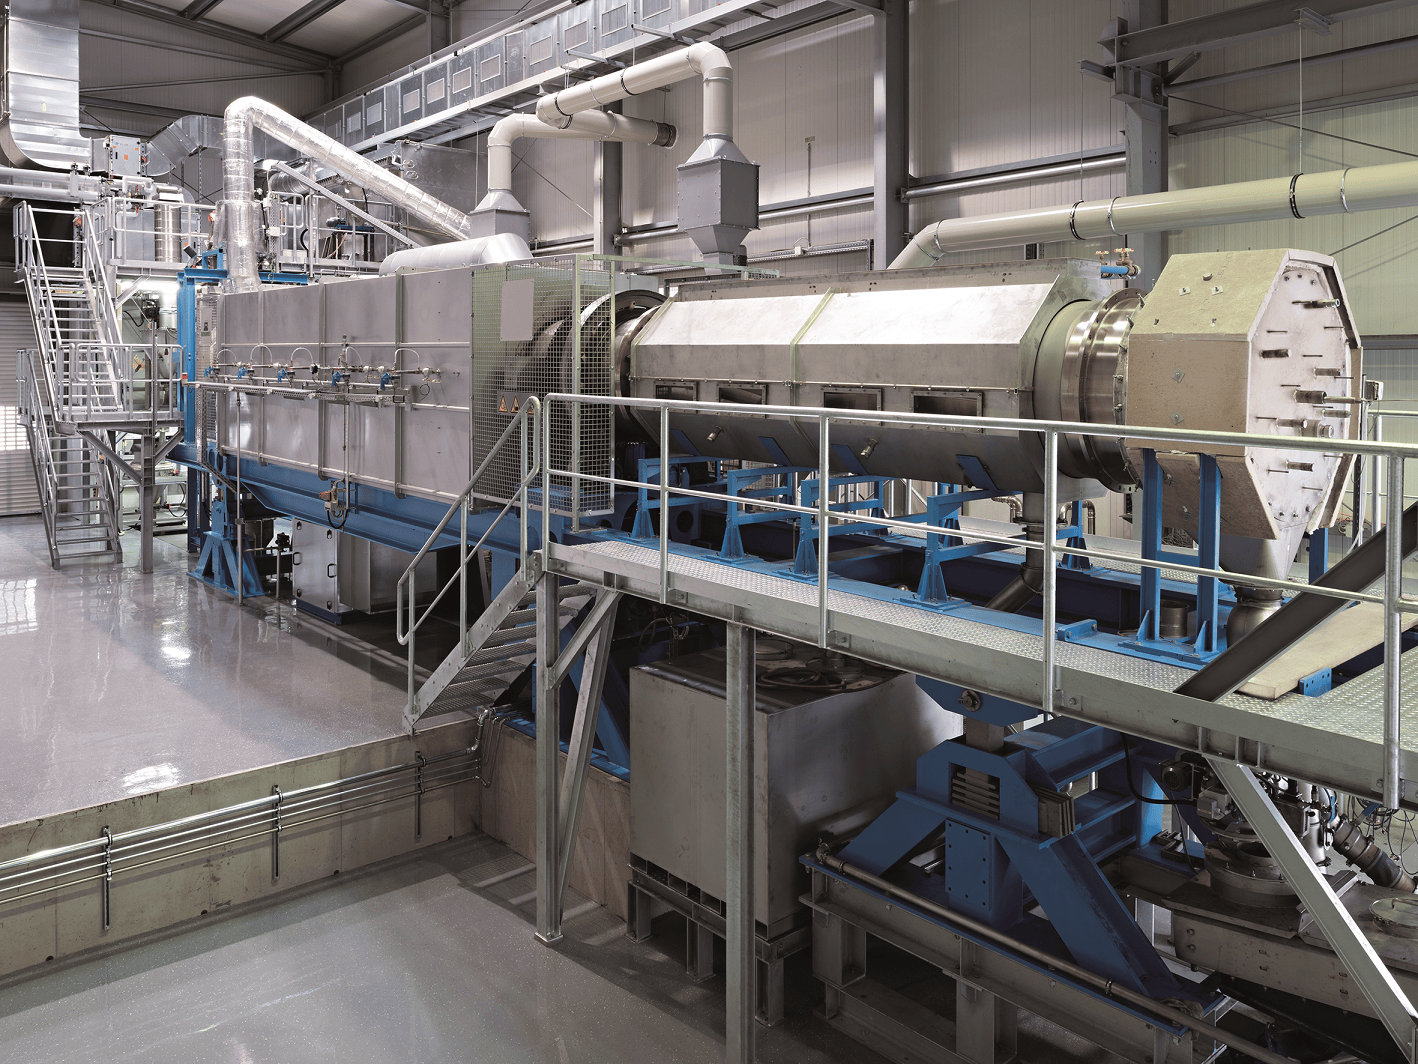 Fully automated inert‑atmosphere system for black mass treatment, removing organics and fluorine at up to 625 °C for clean, safe battery material recovery.
Riedhammer GmbH · Battery Recycling Rotary Kiln
4.3 Battery Materials Separation
- IN
- Battery Shreds
- OUT
- Ferrous Metals
- Aluminum
- Copper
- Plastics (separator)
- Graphite
- Black Mass
- TECH
- Battery Recycling Filter Press:
- sieves
- air classification
- milling
- magnetic separation
- eddy current separation
- density separation
- filtration
- flotation
EA Partner Solutions: MSE Filterpressen GmbH
Once the shreds have been dried, the mechanical sorting and separation process begins. This step focuses on systematically separating and removing all impurities from the cathode active materials. These impurities may include plastics, organics, stainless steel/steel, aluminum, copper, residual traces of WEEE (electronic waste), electrolyte solvents and salts, and possibly graphite.
Technologies that may be applied include sieves, air classification (zig-zag sifter), milling, magnetic separation, eddy current separation, density separation, filtration, and flotation.
Field challenges
Defining the desired level of separation
Decisions must be made about how pure each separated stream needs to be. For example, is it sufficient to recover a mixed metal fraction, or should ferrous metals, aluminum, and copper be separated individually? Higher purity increases the complexity, cost, and energy demand of processing. A cost-benefit analysis should guide these decisions to balance recovery quality with operational efficiency.
Increasing selectivity while minimizing losses
Each separated material stream results in some loss of valuable cathode active materials—often in very small amounts. The challenge lies in maximizing impurity removal while keeping these losses to an absolute minimum.
Maintaining process efficiency with innconsistent feedstock
The composition of input batteries vary in materials used, leading to fluctuation in process efficiency and separation quality. The goal is to implement adaptive sorting and separation technologies. This could be either technologies where processing parameters can be adapted easily or potentially AI-driven process controls. In any case – pre-sorting batteries by chemistry and processing same batteries in one campaign helps reduce variability and enhance process stability.
Solution for this step
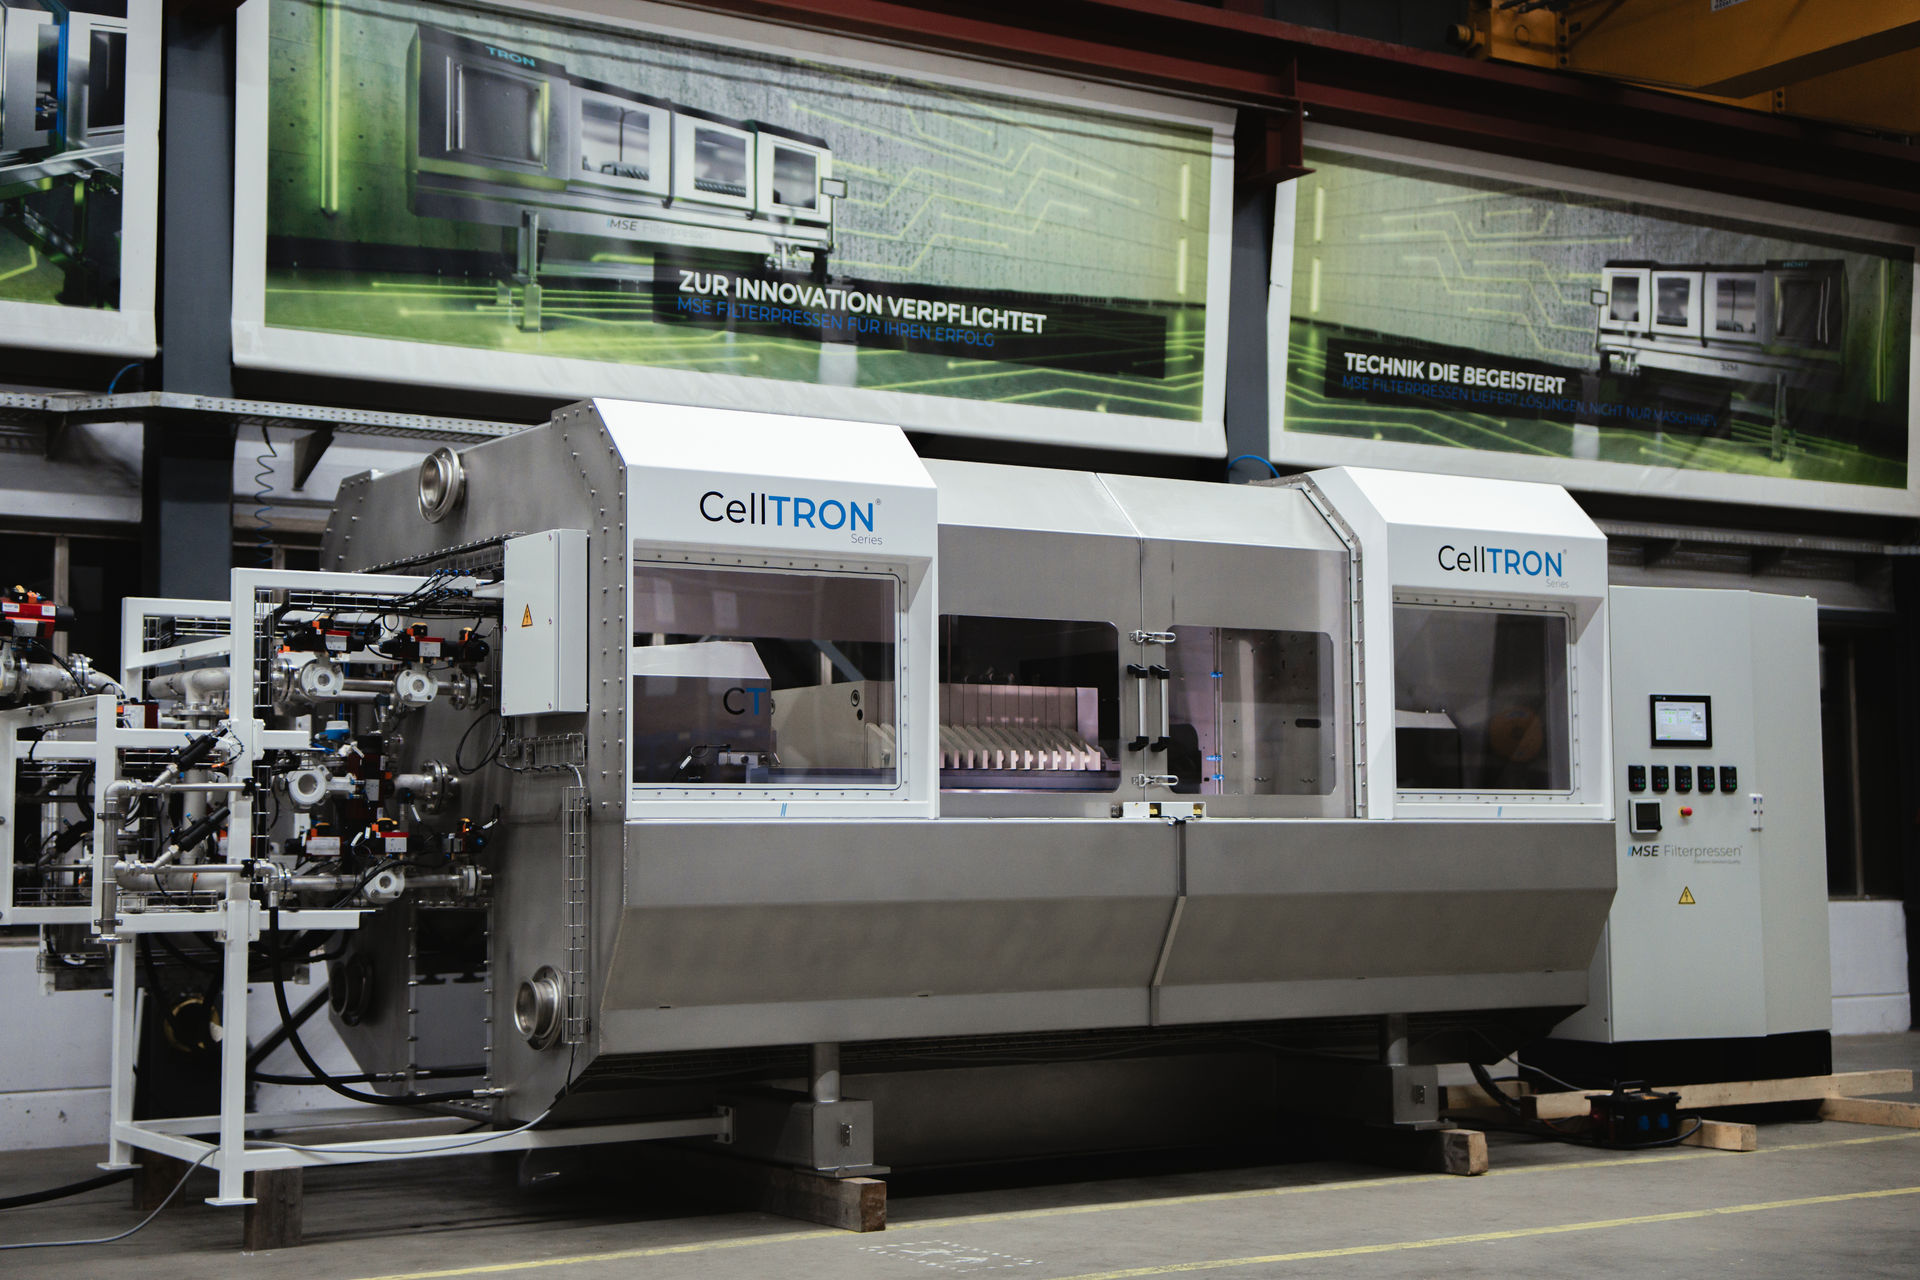
Advanced Filter Press Technology CellTRON
Fully automated filter press process with innovative CIP system and enclosureMSE Filterpressen GmbH · Battery Recycling Filter Press
Solutions for the full Mechanical Battery Recycling stage

ANDRITZ Battery Recycling Solution
ANDRITZ's mechanical pre-treatment for battery recycling uses Duesenfeld's low-temperature process to efficiently shred, dry, and separate Li-ion batteries, maximizing black mass & material recovery.ANDRITZ AG · Turnkey line for this stage
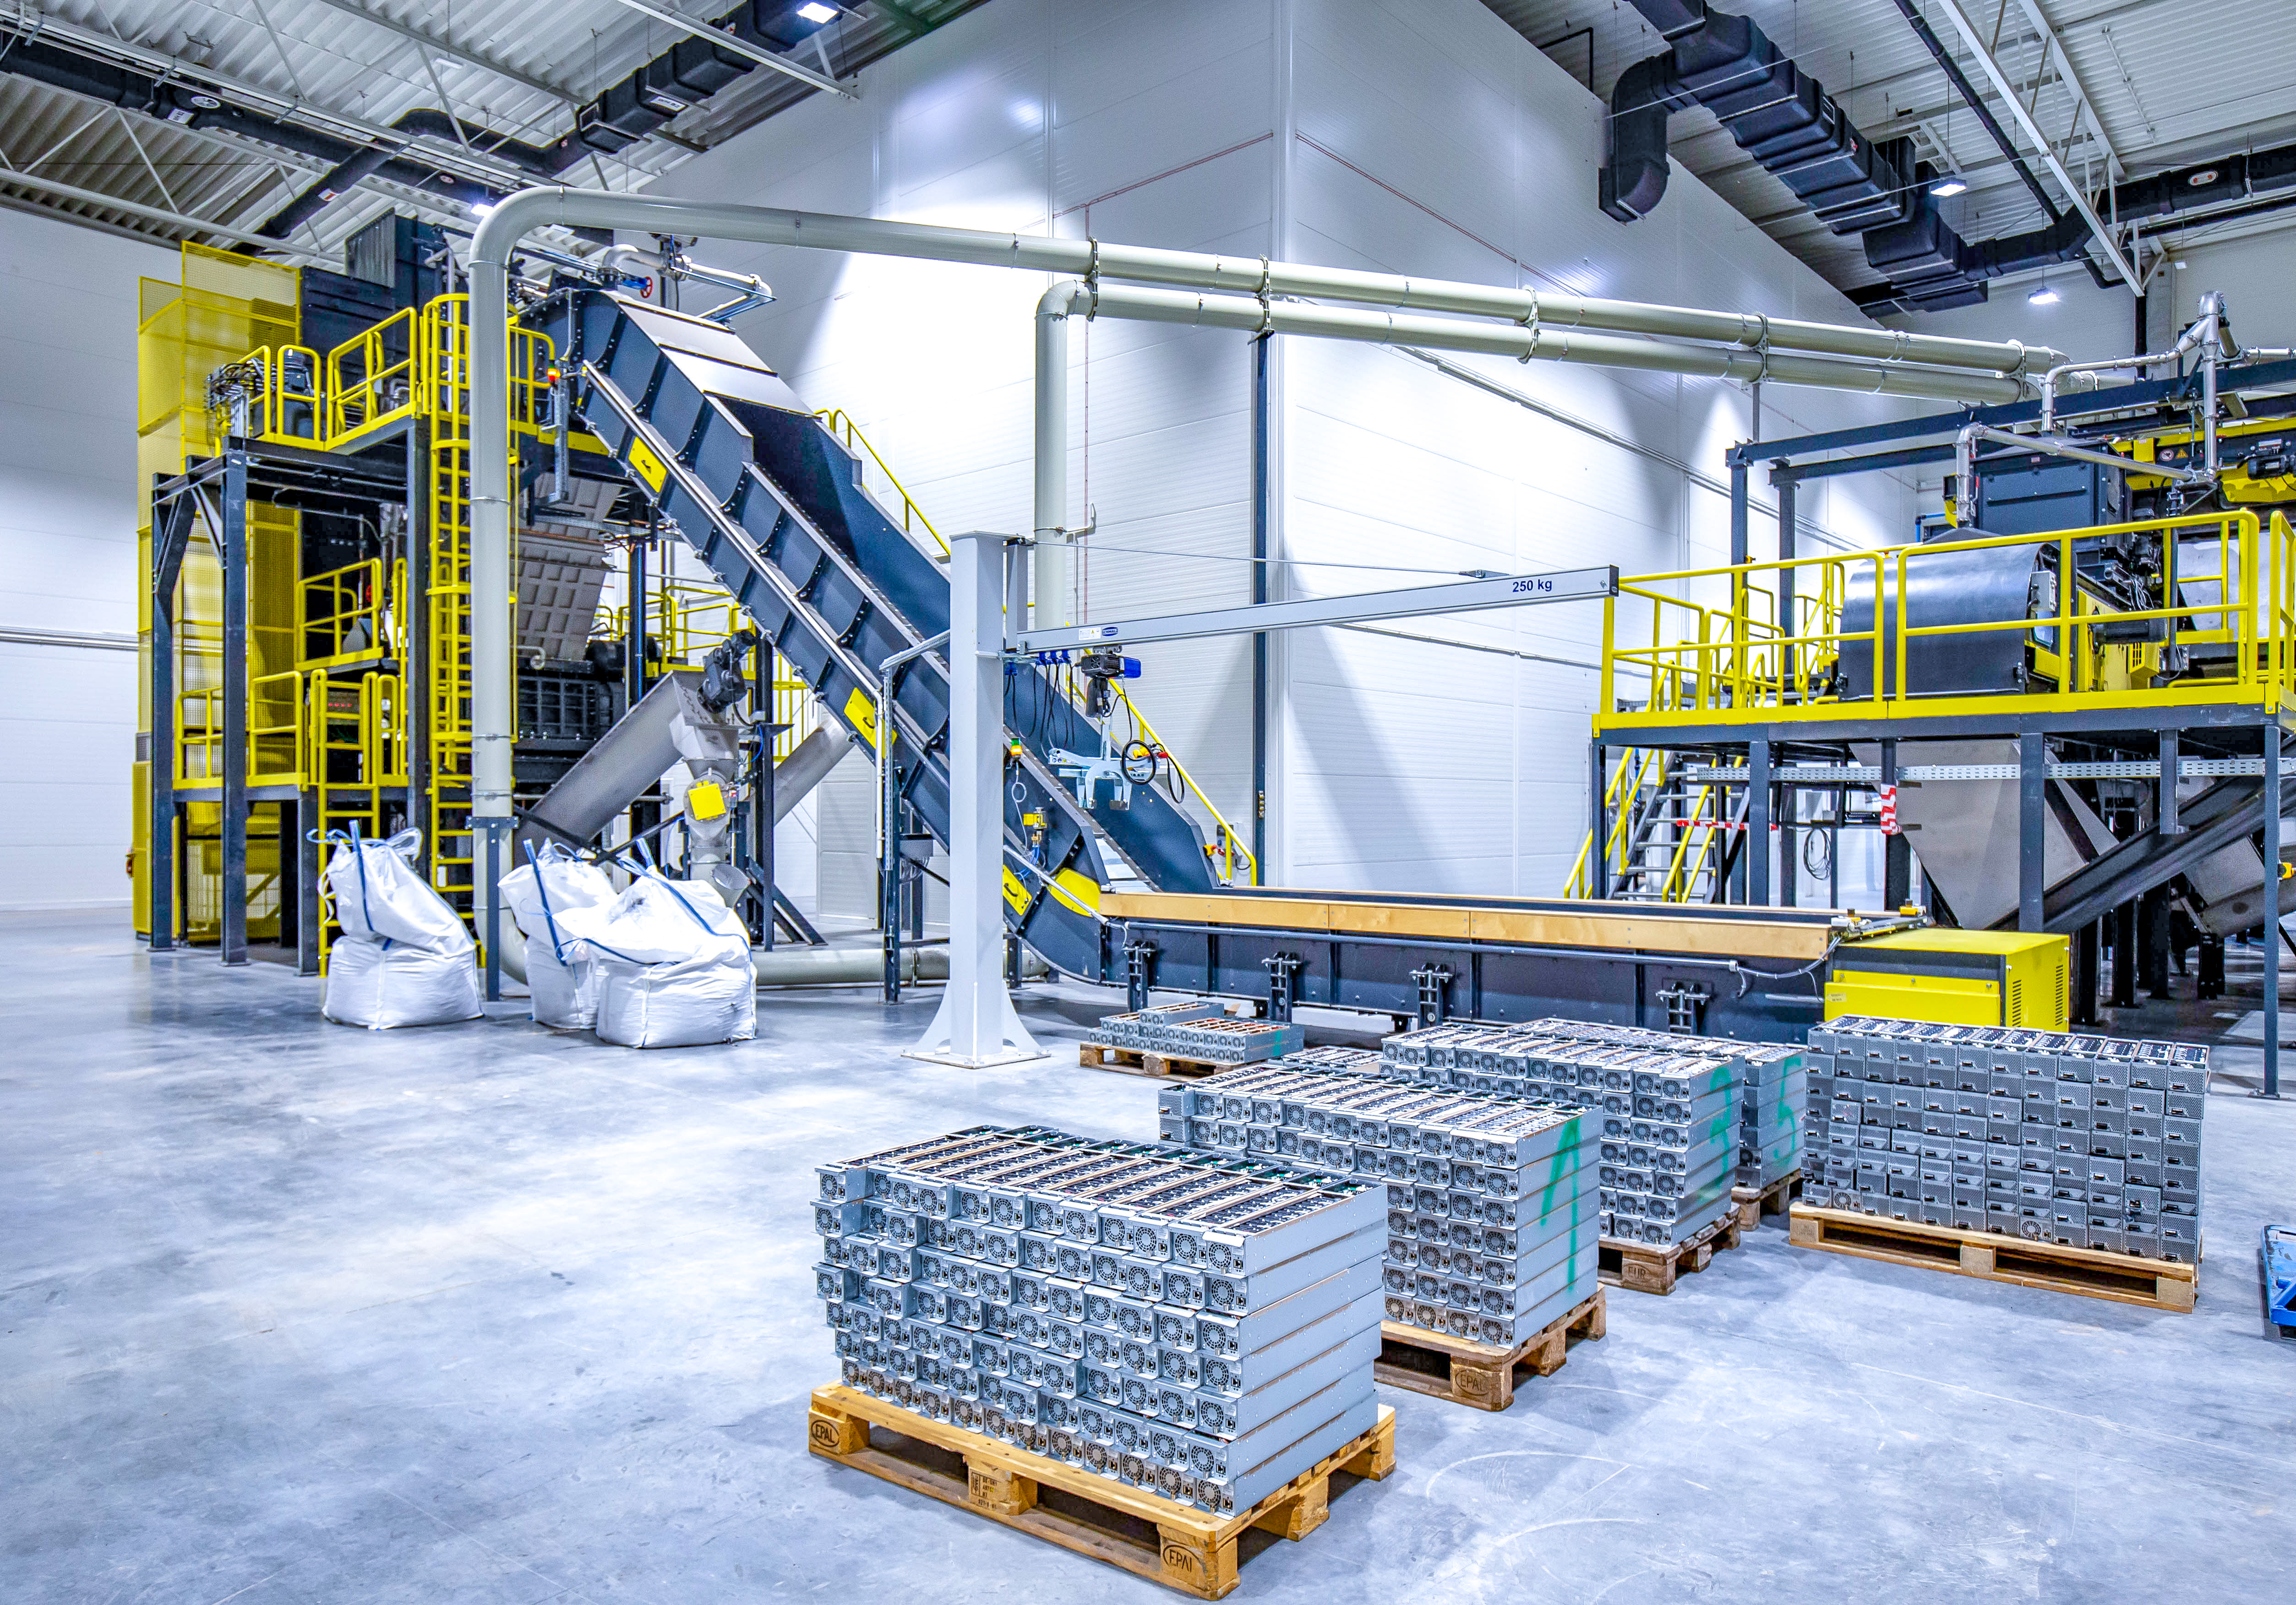
URT Lithium-Ion-Battery Recycling Plant
URT develops and delivers turnkey recycling plants for lithium-ion batteries with a strong focus on depollution, process safety and regulatory compliance. Over 98% black mass recovery.URT Umwelt- und Recyclingtechnik · Turnkey line for this stage
Questions answered
What’s the best way to minimize impurities and maximize black mass yield?
Maximizing black mass yield while minimizing impurities requires careful control of the shredding and separation processes. Factors such as knife type, rotation speed, and shredding atmosphere affect the degree of contamination from copper, aluminum, or plastics. Process optimization and equipment design are key to improving material purity and overall recovery efficiency.
How can electrolyte be removed effectively and with low energy use?
Removing electrolyte efficiently while minimizing energy consumption involves selecting appropriate drying technologies. Methods such as vacuum drying or pyrolysis can be optimized for lower energy input while still achieving complete electrolyte removal. The main challenge is finding the right balance between thorough removal and energy efficiency.
How can batteries be shredded safely without risking fire or explosion?
Safely shredding batteries involves several precautions to prevent hazards such as fire. One method is to discharge the batteries beforehand to reduce stored energy. Another approach is to use a cooling medium, such as water or cryogenic shredding, to lower temperatures and prevent ignition. Additionally, water can help suppress sparks. However, the optimal combination of discharge, water, nitrogen, or cryogenic conditions must be evaluated based on the feedstock and operational targets.
Guidelines & Regulations
The Governmental Regulations section outlines key policies and legal frameworks that govern battery production, usage, recycling, and disposal to ensure safety, sustainability, and compliance with environmental standards.
Industrial Emissions DirectiveEuropean Commission
Sets pollution limits (air, water, and land) for industrial installations. Shredding and pre-treatment facilities that process more than 75 tonnes per day fall under its scope. To obtain permits, these facilities must stay below emission thresholds for regulated pollutants, as defined by the Best Available Techniques (BAT) documents. The BAT reference document for waste treatment was published in 2018.
Waste Framework Directive (WFD)European Commission
This is the foundational waste framework in the EU, defining what constitutes hazardous waste (including lithium-ion batteries) and setting rules for its transport, storage, and treatment. Every company involved in the treatment of hazardous waste must obtain a permit from a national authority to operate and is subject to periodic inspections. These companies are also required to keep records of the quantity and nature of the waste or recycled products, as well as the treatment methods used.
EU Battery RegulationEuropean Commission
Rules around material separation include: removal of all fluids and acids, separation of mercury, where applicable, and separation of cadmium, where applicable. Special precautions and safety measures must be in place for the treatment of waste lithium-based batteries, including protection from excessive heat, water, crushing, or physical damage. Lithium-ion batteries may not be crushed or subjected to energy recovery. However, the exact method of material separation is not prescribed by the regulation.
Universal Waste Regulation (UWR)US EPA
The UWR simplifies the management of certain hazardous wastes, including EV batteries, during material separation stages. It allows for easier collection, storage, and transportation before processing. Under UWR, EV batteries are exempt from some of the stricter hazardous waste requirements, reducing the regulatory burden on facilities involved in storage and separation. The regulation still ensures safe handling to prevent leaks, spills, and environmental risks while the batteries await further processing.
National Pollutant Release Inventory (NPRI)CEPA
The NPRI tracks pollutants released during material separation, requiring facilities to report emissions of hazardous substances such as mercury, lead, and cadmium. This helps ensure that material recovery processes do not lead to environmental pollution and that operations remain in compliance with Canada’s environmental standards for hazardous materials.
Note: This section does not represent a complete or exhaustive overview of all applicable regulations. It is intended for general orientation only and should not be considered legal advice or regulatory interpretation. For detailed compliance guidance, always consult the official legislation or a qualified regulatory expert.
Innovation & trends
Direct recycling
Direct recycling technologies aim to recover and reuse intact battery components—such as cathode materials—without dissolving them into base elements. By skipping the chemical-intensive steps of hydrometallurgy, direct recycling can significantly reduce energy use, preserve material structure, and lower environmental impact. While still emerging, this approach shows strong potential for high-performance material recovery.
Advanced safety functions in shredding
Recent innovations in battery shredding focus on enhanced safety systems to minimize the risk of fire and thermal events. These include water baths, chemical suppression systems, and inert atmosphere shredding, all of which help control heat buildup and prevent ignition during the process.
Recommended papers
Shredding of Lithium-Ion Batteries: Overview and Industrial Perspective
Summarizes key shredding methods used in battery recycling, including safety measures, process environments.- Recovering electrolyte at different temperatures – off-gas analysis
- Research approach to recover electrolyte
- Deeper discharge increases impurities in black mass, challenging flotation and recovery steps.